
INJ-01
2h 14min 05sRunning
OEE87,4
- D96,1%
- P93,8%
- Q97,0%
312,411,5 s2.946
OP 2470·Handle 128 mm
- Scrap
- 38
- Good
- Exp.
- 3.120
Track your whole production in real time and know where to act to improve.
Loading the 3D factory…
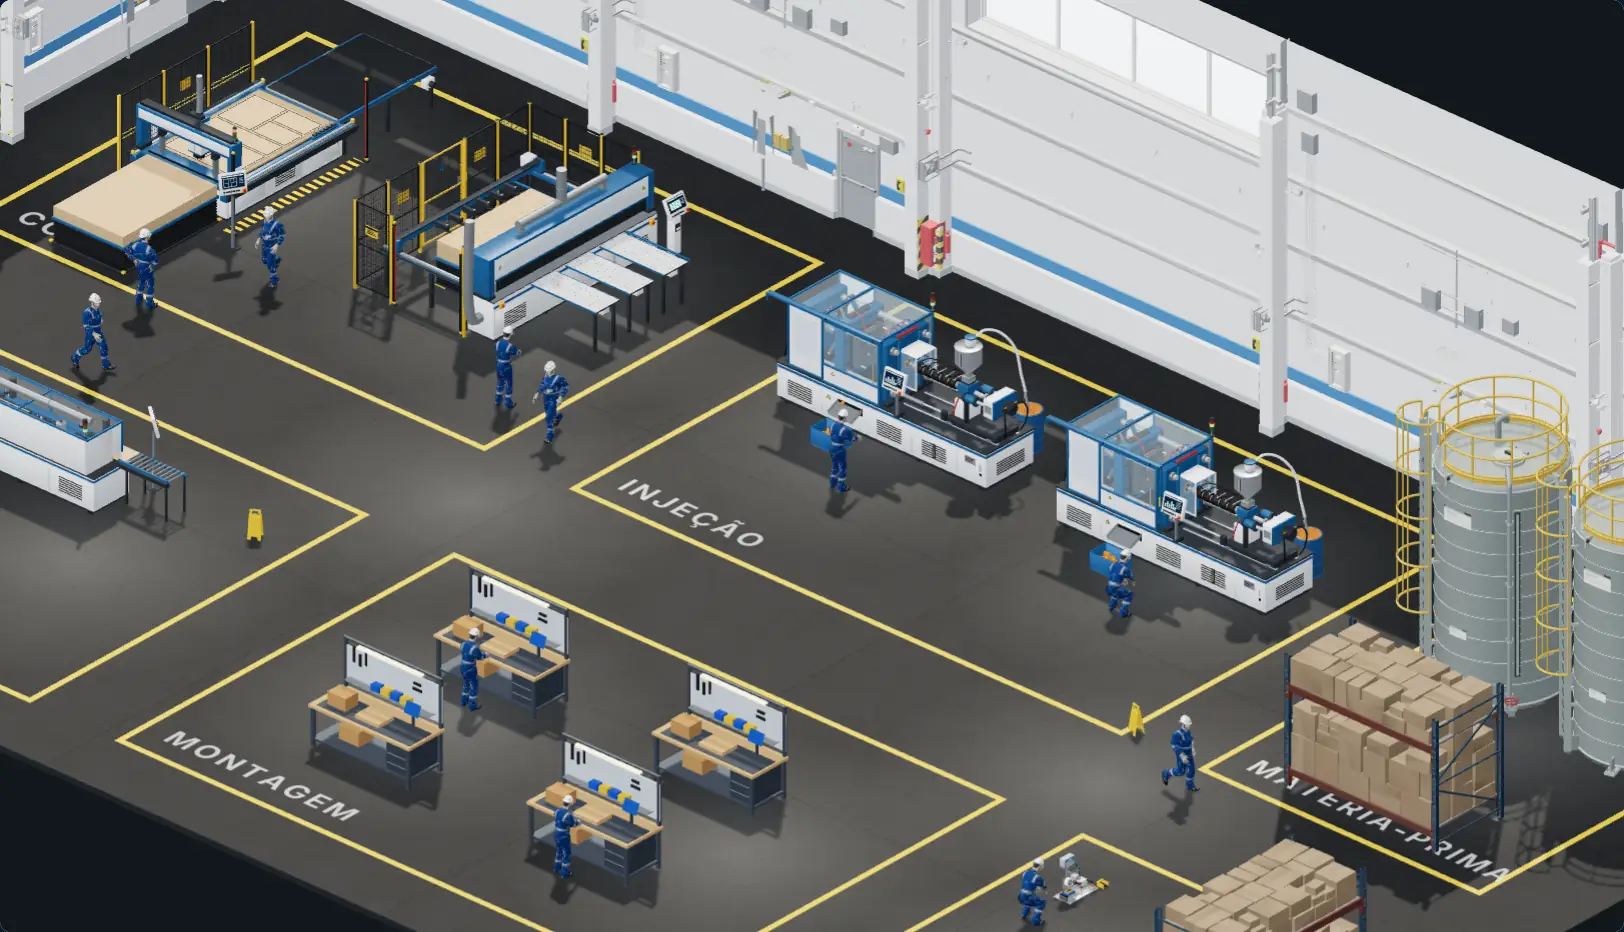
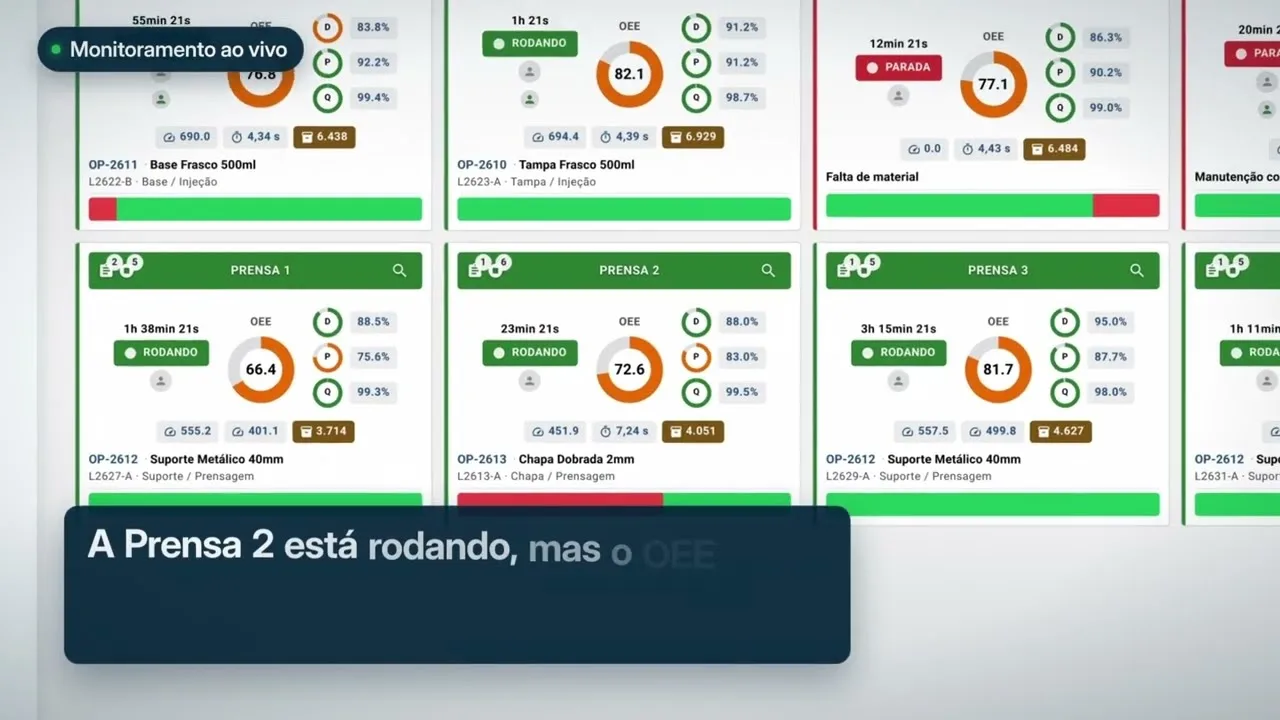
The model shows a furniture plant with plastic injection: cutting, edging and drilling, injection, assembly, raw material and shipping. Each machine shows its state, how long it has been in it, the stop reason, the running order, the queue and its OEE.
Already producing with Mestti
On video
Understand Mestti in 1 minute.
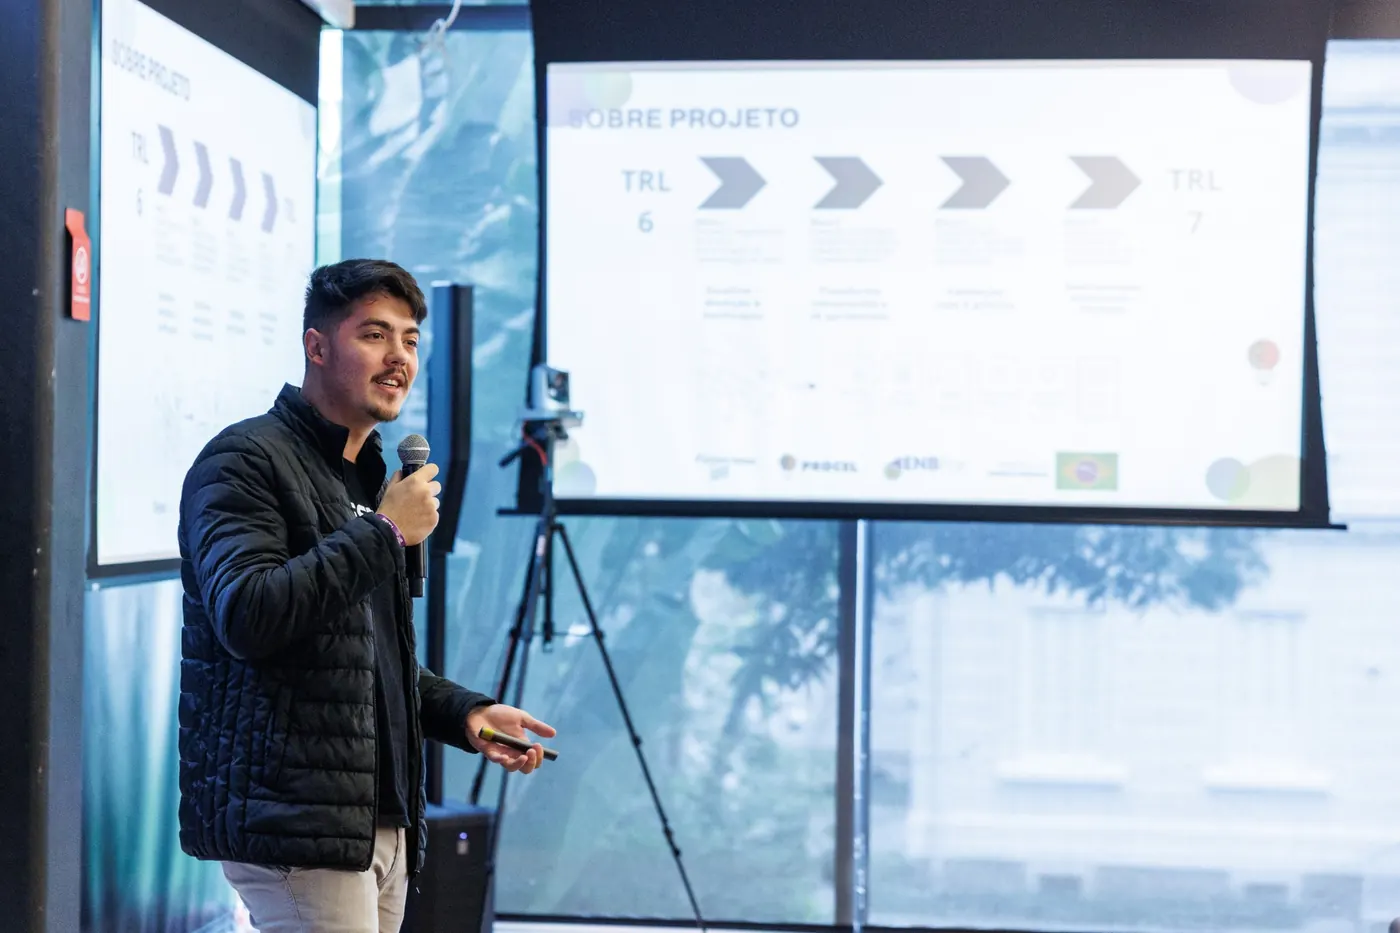
News · Lab Procel II
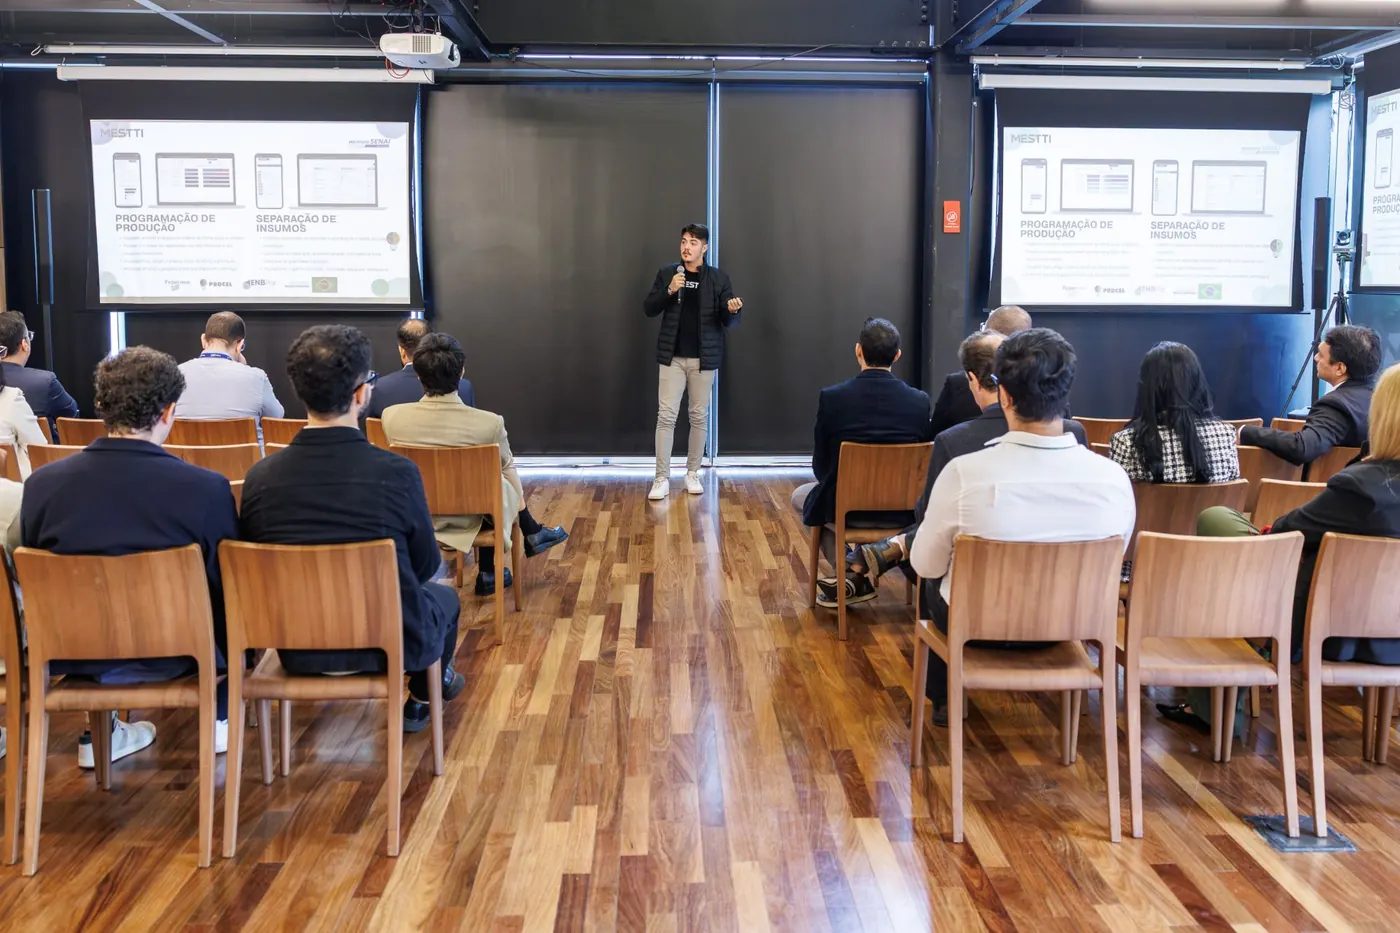
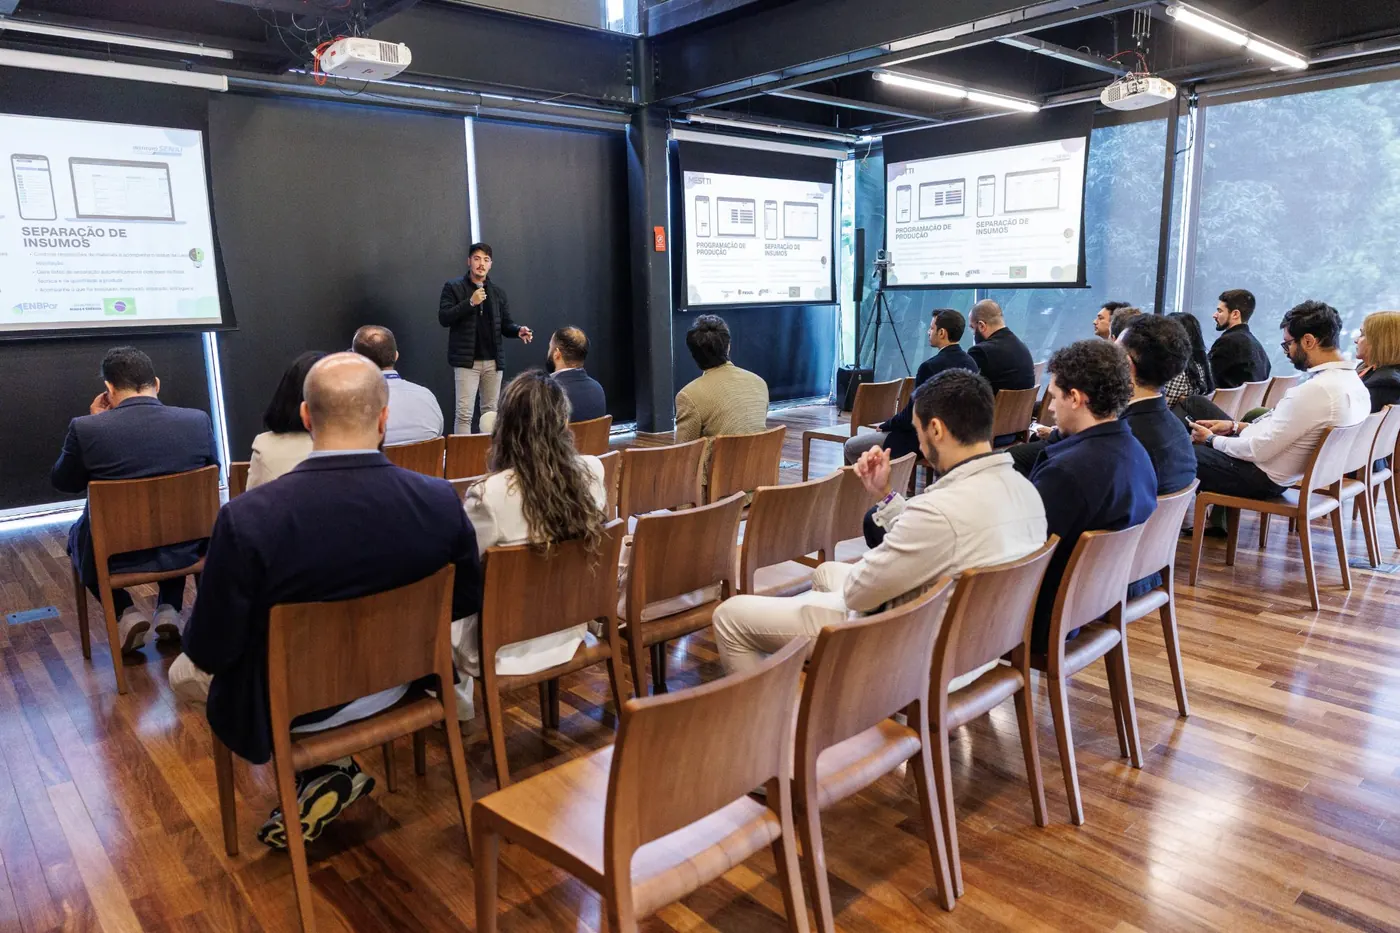
The only startup from southern Brazil selected for Lab Procel II, the federal energy efficiency innovation program run by ENBPar with SENAI Rio de Janeiro.
 Read the news on ENBPar
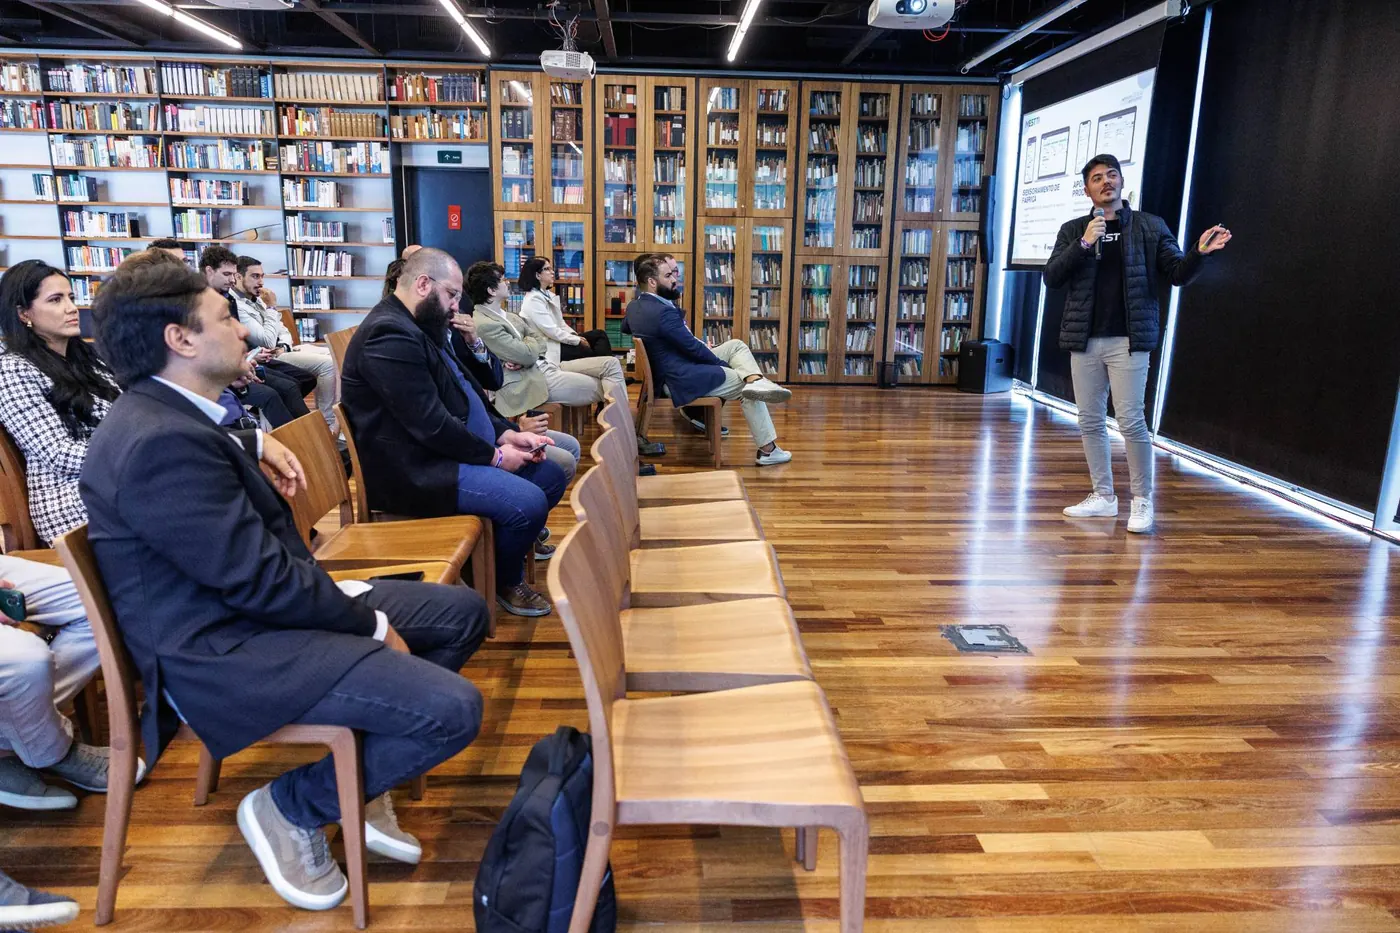
Mestti was born in a factory with these problems.
Owners and directors
“We could produce more. I just don’t know where we’re losing it.”Per-machine monitoring
Planning
“I only find out about delays on the delivery date.”Scheduling with expected dates
Supervisors
“Holding the team accountable always turns into an argument.”Stops with reason and time
Quality
“A customer sent parts back and I can’t prove the inspection.”Inspections with photo and name
IoT sensors send each machine’s telemetry, new or old, to Mestti in real time, and AI helps read that data. That is how Industry 4.0 reaches the factory floor.
Product, components and routing: which machine runs each step, cycle time, parts per cycle and setup. This record sets each machine’s target, the schedule and the cost per product.
Component · Side panel 18 mm 2100 × 550 2 parts/product
| Step | Machine | Cycle | Setup | Cost/product |
|---|---|---|---|---|
| 1 · Cutting | SEC-01 | 42 s | 15 min | R$ 3,80 |
| 2 · Edge banding | COL-01 | 35 s | 20 min | R$ 4,10 |
| 3 · Drilling | FUR-01 | 28 s | 10 min | R$ 2,20 |
Component · Handle 128 mm 3 parts/product
| 1 · Injection | INJ-01 | 28 s · 4 parts/cycle | 40 min | R$ 0,90 |
The order joins the machine queue with start and end calculated from the routing and real capacity. If the delivery doesn’t close, the delay shows up in the schedule before production starts.
OP 2503 ends tomorrow 4:40 p.m. Due tomorrow 12:00: 4h40 late.
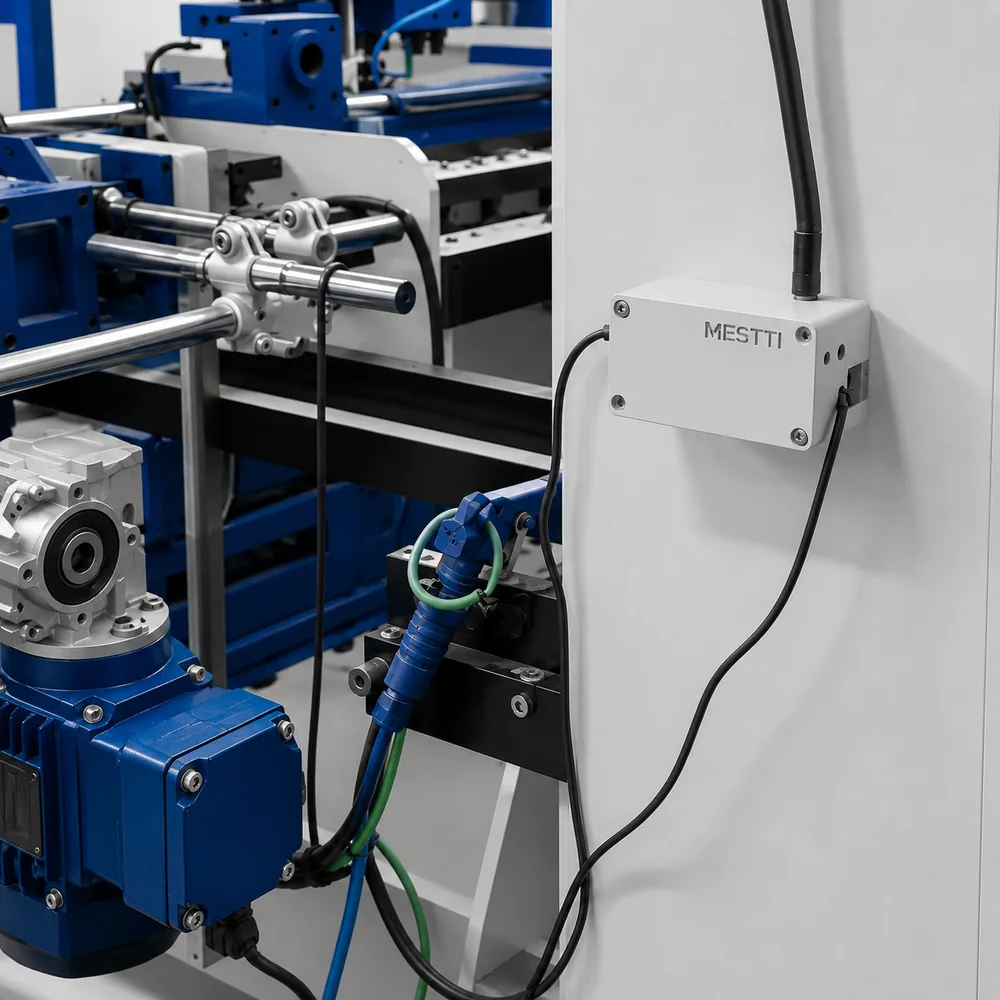
IoT sensor installed without touching the PLC. It counts every cycle and logs stops and micro-stops on its own; the telemetry reaches Mestti in 4 seconds. Where there is no sensor, such as benches and assembly, the operator logs it on the tablet: start, pause, finish and quantity.
OP 2470·Handle 128 mm
Material shortage
The inspector fills in the checklist on the phone, with measurement, photo and name. A measurement out of tolerance becomes non-conforming. Everything is kept for audits and customer answers.
Pending 2
In progress 1
Done 14
At the end of the shift: 2,946 of 3,120 parts.
1h40 stopped for lack of material.
Without stopping production or touching the PLC.
+20%
At a furniture customer, the sensor showed the machines spent the start of each shift warming up. Now they are switched on earlier.
Before: machine switched on at 06:00, when the shift starts
After: machine switched on before the shift
The real screens, with a sample factory.
Loading the schedule…
OP 2470·Handle 128 mm
Material shortage
OP 2488·Drawer organizer
OP 2479·Drilled wardrobe side
CNC-02 · Panel cutting · Shift A
0 / 3
AI-powered platform
Otto is Mestti’s artificial intelligence agent. He works with your real production data, within each user’s permissions, and only carries out an action after someone approves it.
Where did I lose the most time this week?
In Panel cutting: 6h40 of stops. 58% were material shortages on CNC-02, almost always between 9 and 10 a.m.
I suggest staging the shift’s boards first thing in the morning.
Which orders could be late?
3 orders finish after their due date. Order 1482 depends on Injection 02, which is 2 h behind plan.
I simulated swapping it with order 1490 and both deliver on time.
What is pending in quality?
2 first-article inspections were not done on the morning shift, on Press 01 and Lathe 01.
One rework non-conformity is waiting for verification.
Differences in rollout, operation and service.
| Traditional MES |  | |
|---|---|---|
| Getting started | Months of project work and consulting | Sensors ready within 7 days. The Mestti team does the rollout at the factory. |
| Machine connection | Integration with each maker’s PLC and protocol | Our own IoT sensor reads the machine signal with no PLC changes. Works on older machines. |
| Production logging | Typed into a terminal or on paper | Automatic from the sensor. Manual on the tablet at stations without a sensor. |
| Data refresh | Depends on manual entry | Within 4 seconds. Without internet, the sensor stores data and sends it when the connection returns. |
| Infrastructure and security | On-site server, backup and security handled by your IT | Cloud. Each company’s data isolated, permission-based access and an immutable original record. |
| Scope | Production only. Engineering and quality live in other systems. | Engineering, planning, production, quality and OEE on one database. Integrates with the ERP. |
| Artificial intelligence | Add-on module | Otto queries the factory data and only runs actions a person has approved. |
| System changes | Quote and vendor queue | Requests reviewed with the customer the same week. New features are tested in a customer’s factory before general release. |
| Relationship | Ticket with the reseller | The team that builds the system visits customers’ factories and talks with management, supervisors and operators. Improvements come from those visits. |
We start with one department.
Together we pick the department that matters most.
Made for your machines.
Sensor on the machine and app on the tablet. No changes to the controls.
Mestti measures the real routine. The team learns by using it.
Hours lost, causes and cost. Not continuing? We remove the sensors at no cost.
It is the first step. No commitment.
Brazilian technology
IoT sensor, MES software and AI agents built in Brazil, by the team that serves your factory.
Selected by Lab Procel, a federal innovation program.
Backed by
It depends on the number of machines and what you will use. The trial week is free and the sensor is on loan. At the end you get a proposal with your numbers. If you don’t continue, we remove the sensors, at no cost and with no commitment.
A Brazilian production management system for manufacturers of every size. Its own sensors measure every machine, and engineering, planning, the shop floor and quality use the same data.
Sensors ready within 7 days, installation in 1 day and a 1-week free trial before you decide.
No. The sensor counts parts and sees whether the machine is running or stopped. It doesn’t watch people. Whoever was at the machine gives the reason for the stop, under their own name.
No. Mestti connects to your ERP: orders come from it and production goes back to it. The ERP keeps handling orders, purchasing and invoicing.
Yes. The sensor reads the count or the machine’s electrical signal. No PLC needed and no changes to the controls.
Yes. On benches, assembly or machines without a sensor, the operator logs on the tablet: start, pause, finish and quantity. The data goes into the same target, OEE and queue as the machines with sensors.
The sensor stores everything and sends it when the connection returns. Nothing is lost.
Each company’s data is isolated and access is by permission. The original record cannot be changed. Otto only acts after a person approves.
Leave your contact and we will schedule the demo at the best time for you.
Sensors ready within 7 days. Installed in 1 day.
Prefer to talk now? WhatsApp · (43) 99109-5035