

What you can see on each machine
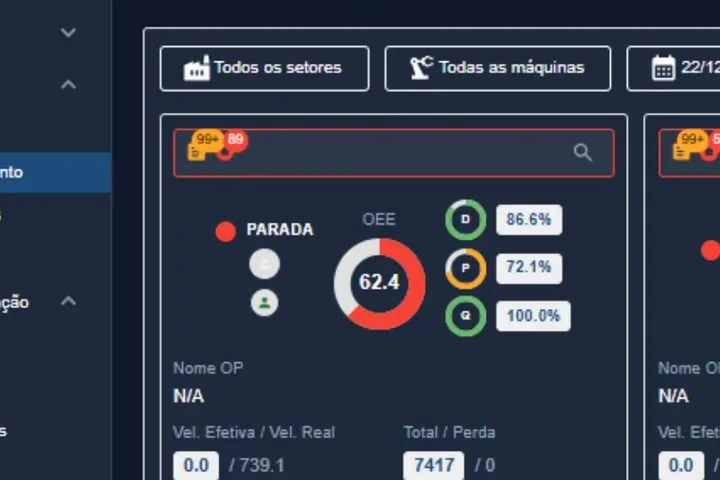
Status and time
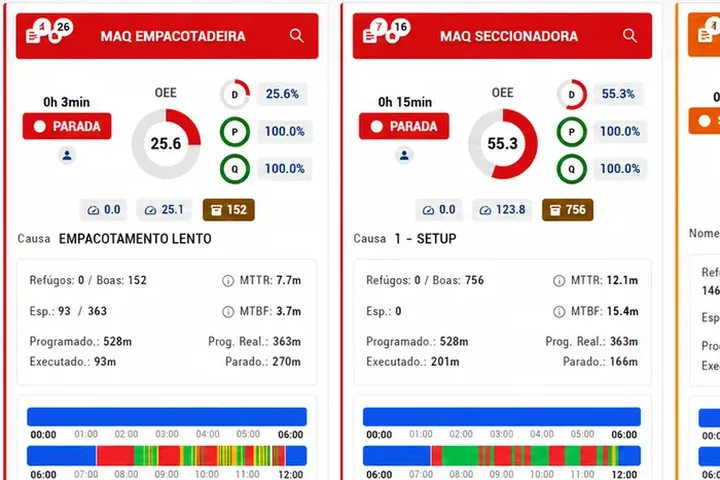
Running, stopped, micro-stop or setup, and for how long.
Production
Parts made, current order and actual cycle compared with the target.
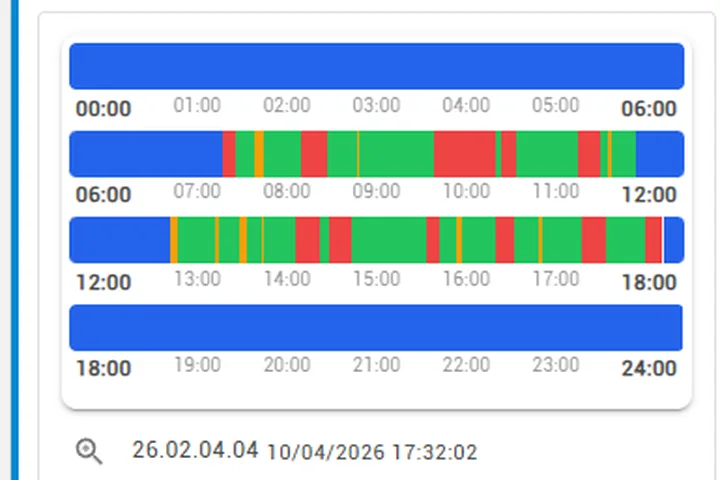
Stops with a reason
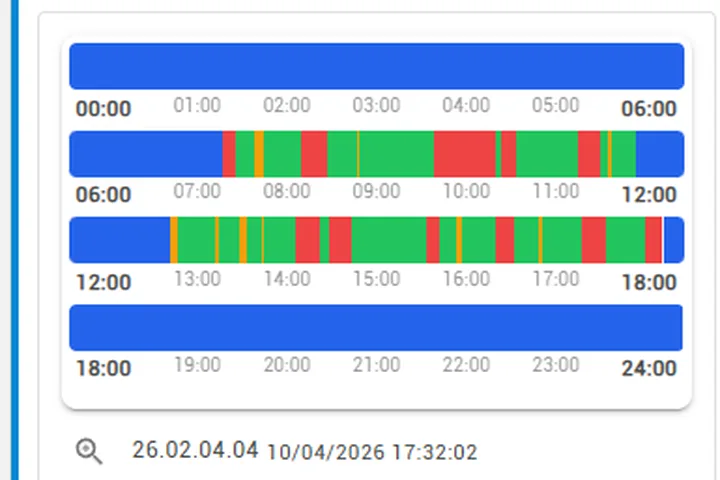
The shift timeline, with the reason for each stop.
OEE and cost
Availability, performance, quality and the lost cost in money.
Walking the floor or a live screen?
Walking around and asking
- You find the stop when you walk past the machine.
- The reason depends on who remembers.
- The day’s total only comes out at closing.
Live monitoring
- The stop shows on screen the minute it starts.
- The reason is entered on the tablet, right away.
- The shift’s OEE and production are always up to date.
Where monitoring usually helps first
Material shortage
The same stop at the same time every day shows up on the timeline.
Long setups
Changeovers that exceed the standard become visible per machine and shift.
Start of the shift
Machines that take long to produce after switching on, as in the furniture case.
Monitoring at Mestti
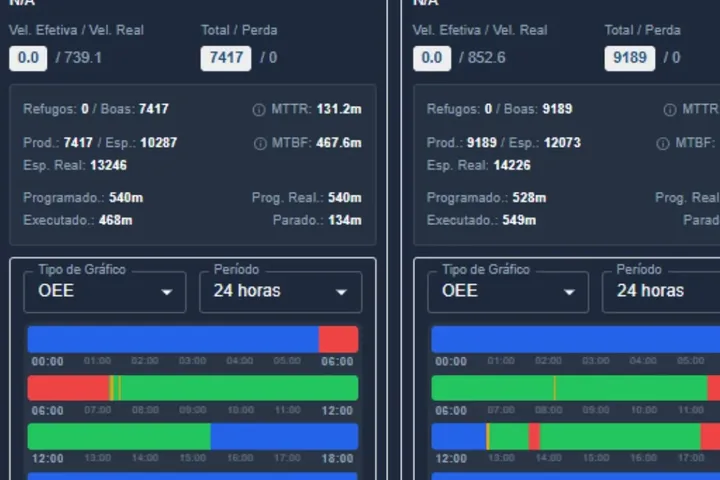
Each machine has a card with status, timer, OEE, current order and the shift timeline.
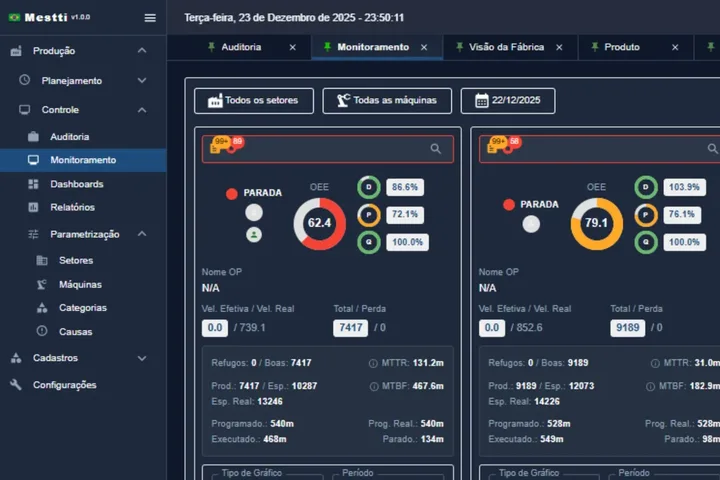
The 4 to 48-hour management view shows how each machine did, where it lost and why.
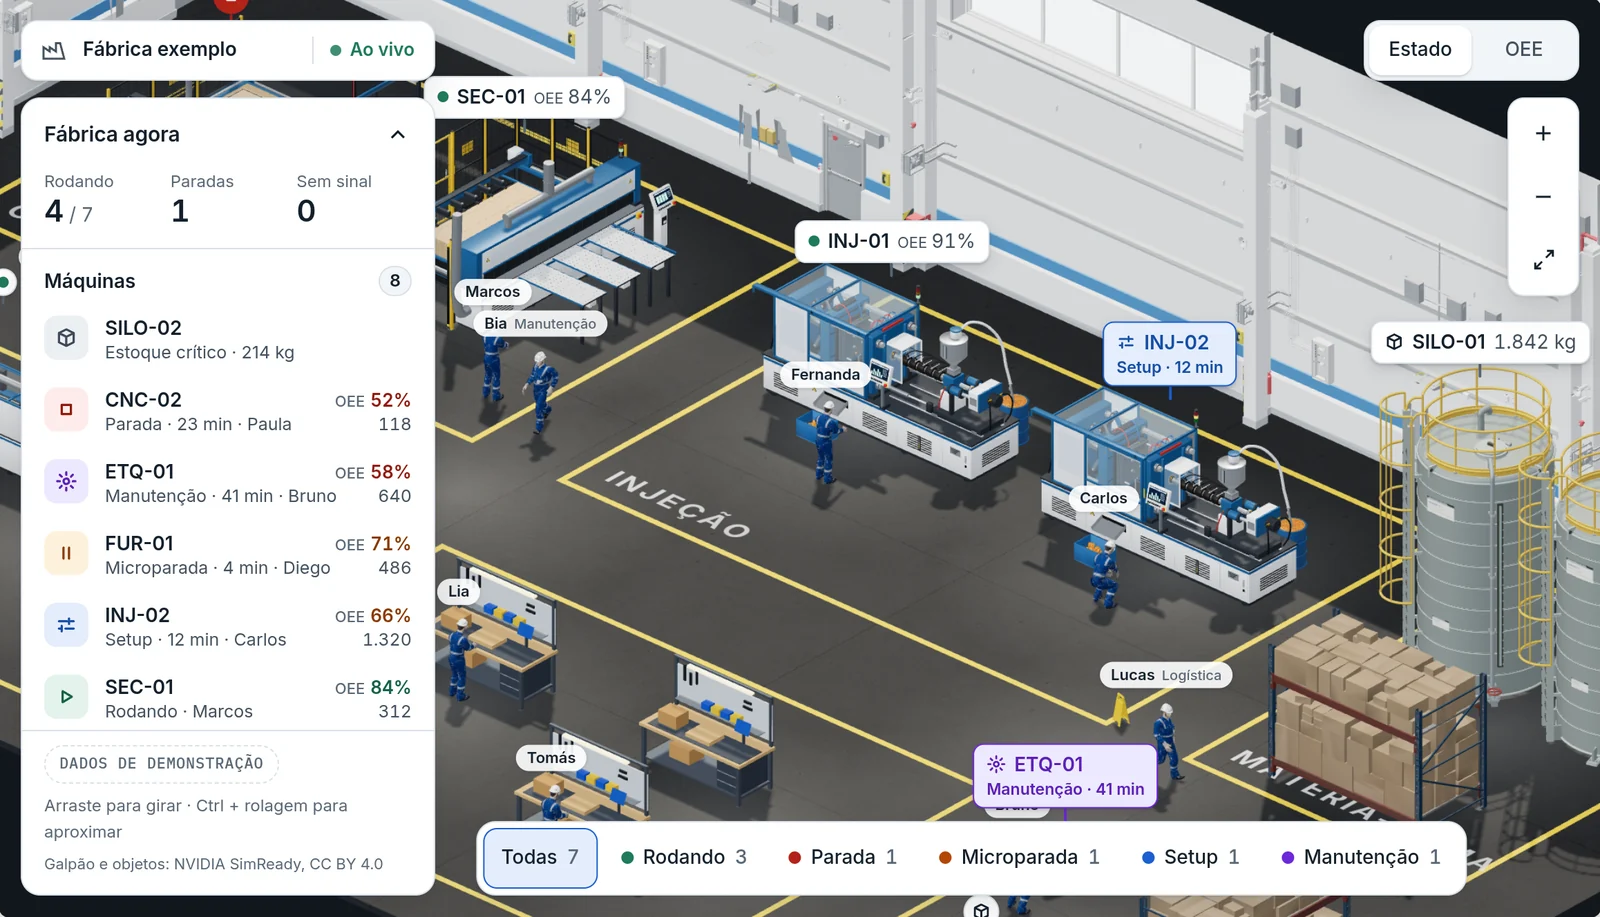
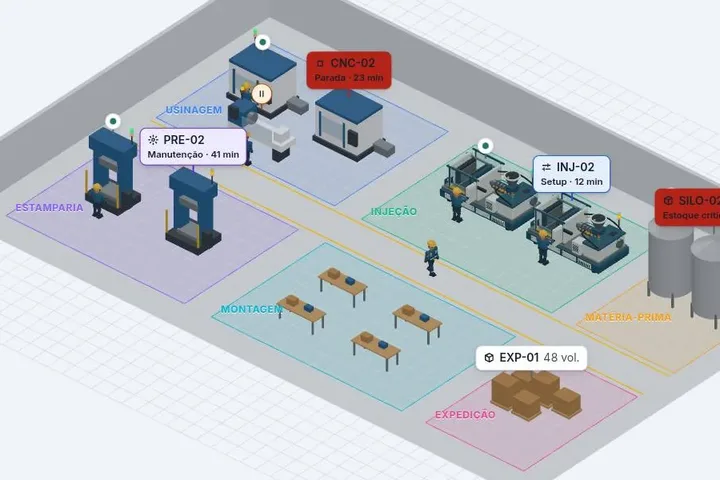
The 3D factory shows every machine’s status on a single screen.
The system opens in the browser, on a computer, phone or a TV on the shop floor.
Questions about monitoring
Does it need internet all the time?
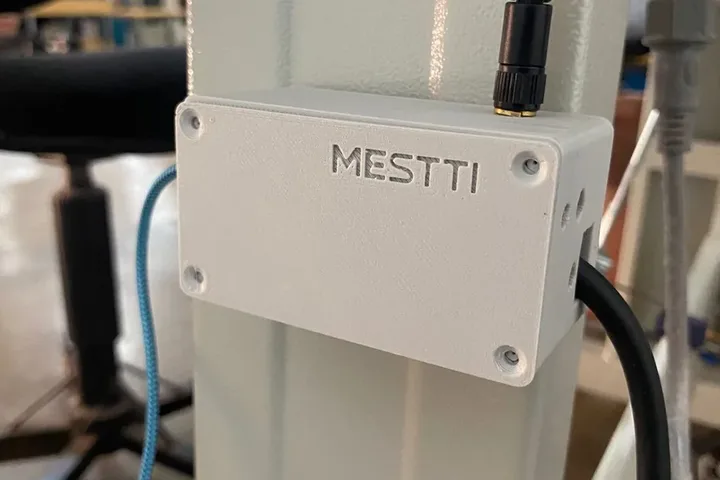
The sensor uses 2.4 GHz Wi‑Fi. If the connection drops, it stores the events and sends them when it returns.
What is a micro-stop?
A short stop, from seconds to a few minutes, that is almost never written down by hand. Added up over a shift, micro-stops can become hours.
Does monitoring watch the operators?
No. The sensor looks at the machine: count and whether it is running or stopped. People add the reason for stops.
Does it work on old machines?
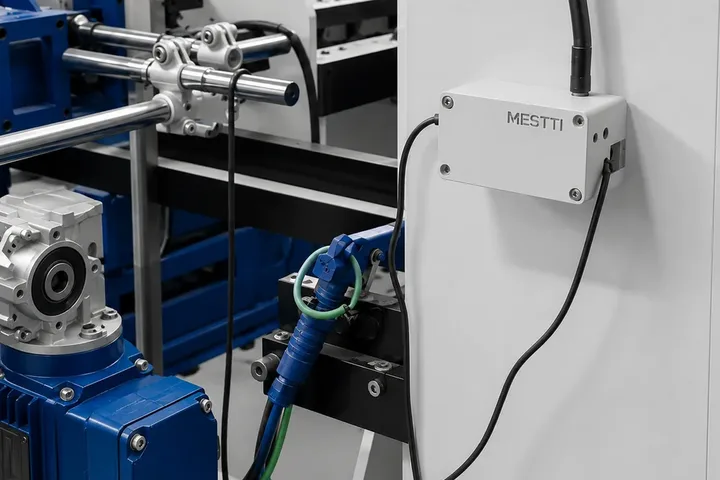
In most cases, yes: the sensor reads count pulses, limit switches, linear measurement or the electrical signal, without a PLC. We assess each machine in the first conversation.
Is it for predictive maintenance?
Mestti focuses on production: count, status and stops. The current signal shows whether the machine is working; it is not vibration analysis. For maintenance, talk to the team about your case.
Articles on this topic (in Portuguese)
 MTBF e MTTR: o que são, como calcular e para que servem
 Motivos de parada de máquina: como montar a lista e registrar no turno
 Microparadas: o que são, quanto custam e como encontrar
 Quanto custa uma hora de máquina parada
 Como reduzir o tempo de setup na prática
 Como escolher um sistema de monitoramento de produção industrial
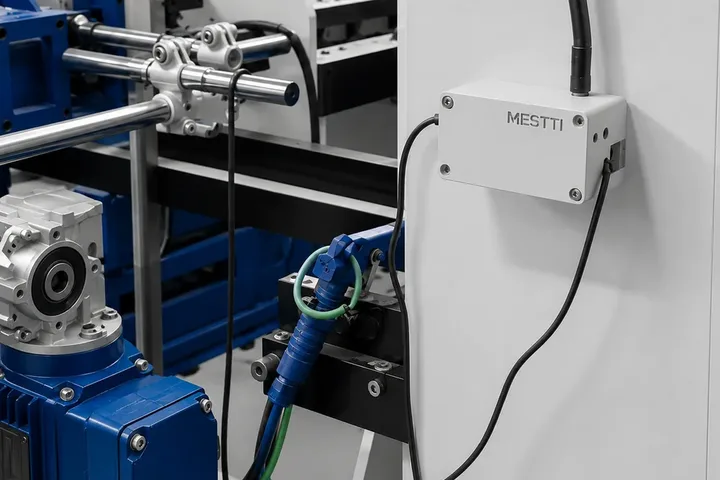 Sensoriamento industrial: como sair do apontamento manual e ter dados em tempo real
Know which machine stopped, why and what it cost.
Leave your contact and we will schedule the demo at the best time for you.
If it does not fit, we remove the sensor and you pay nothing.
Prefer to talk now? WhatsApp · (43) 99109-5035